
Contents
- Understanding Stainless Steel Welding
- Key Considerations for Welding Stainless Steel Grades
- Comparison of Welding Metals
- Stainless Steel Welding Joints
- Stainless Steel Welding Methods
- Stainless Steel Welding Quality Tests
- Common Weld Defects
- Cost Drivers
- Case Study 1 : When stainless steel parts no longer fit
- Case Study 2: When a stainless steel weld repeatedly cracks
- Applications
- Why choose Novelty Structures ?
- How can we help you ?
- FAQ

Understanding Stainless Steel Welding
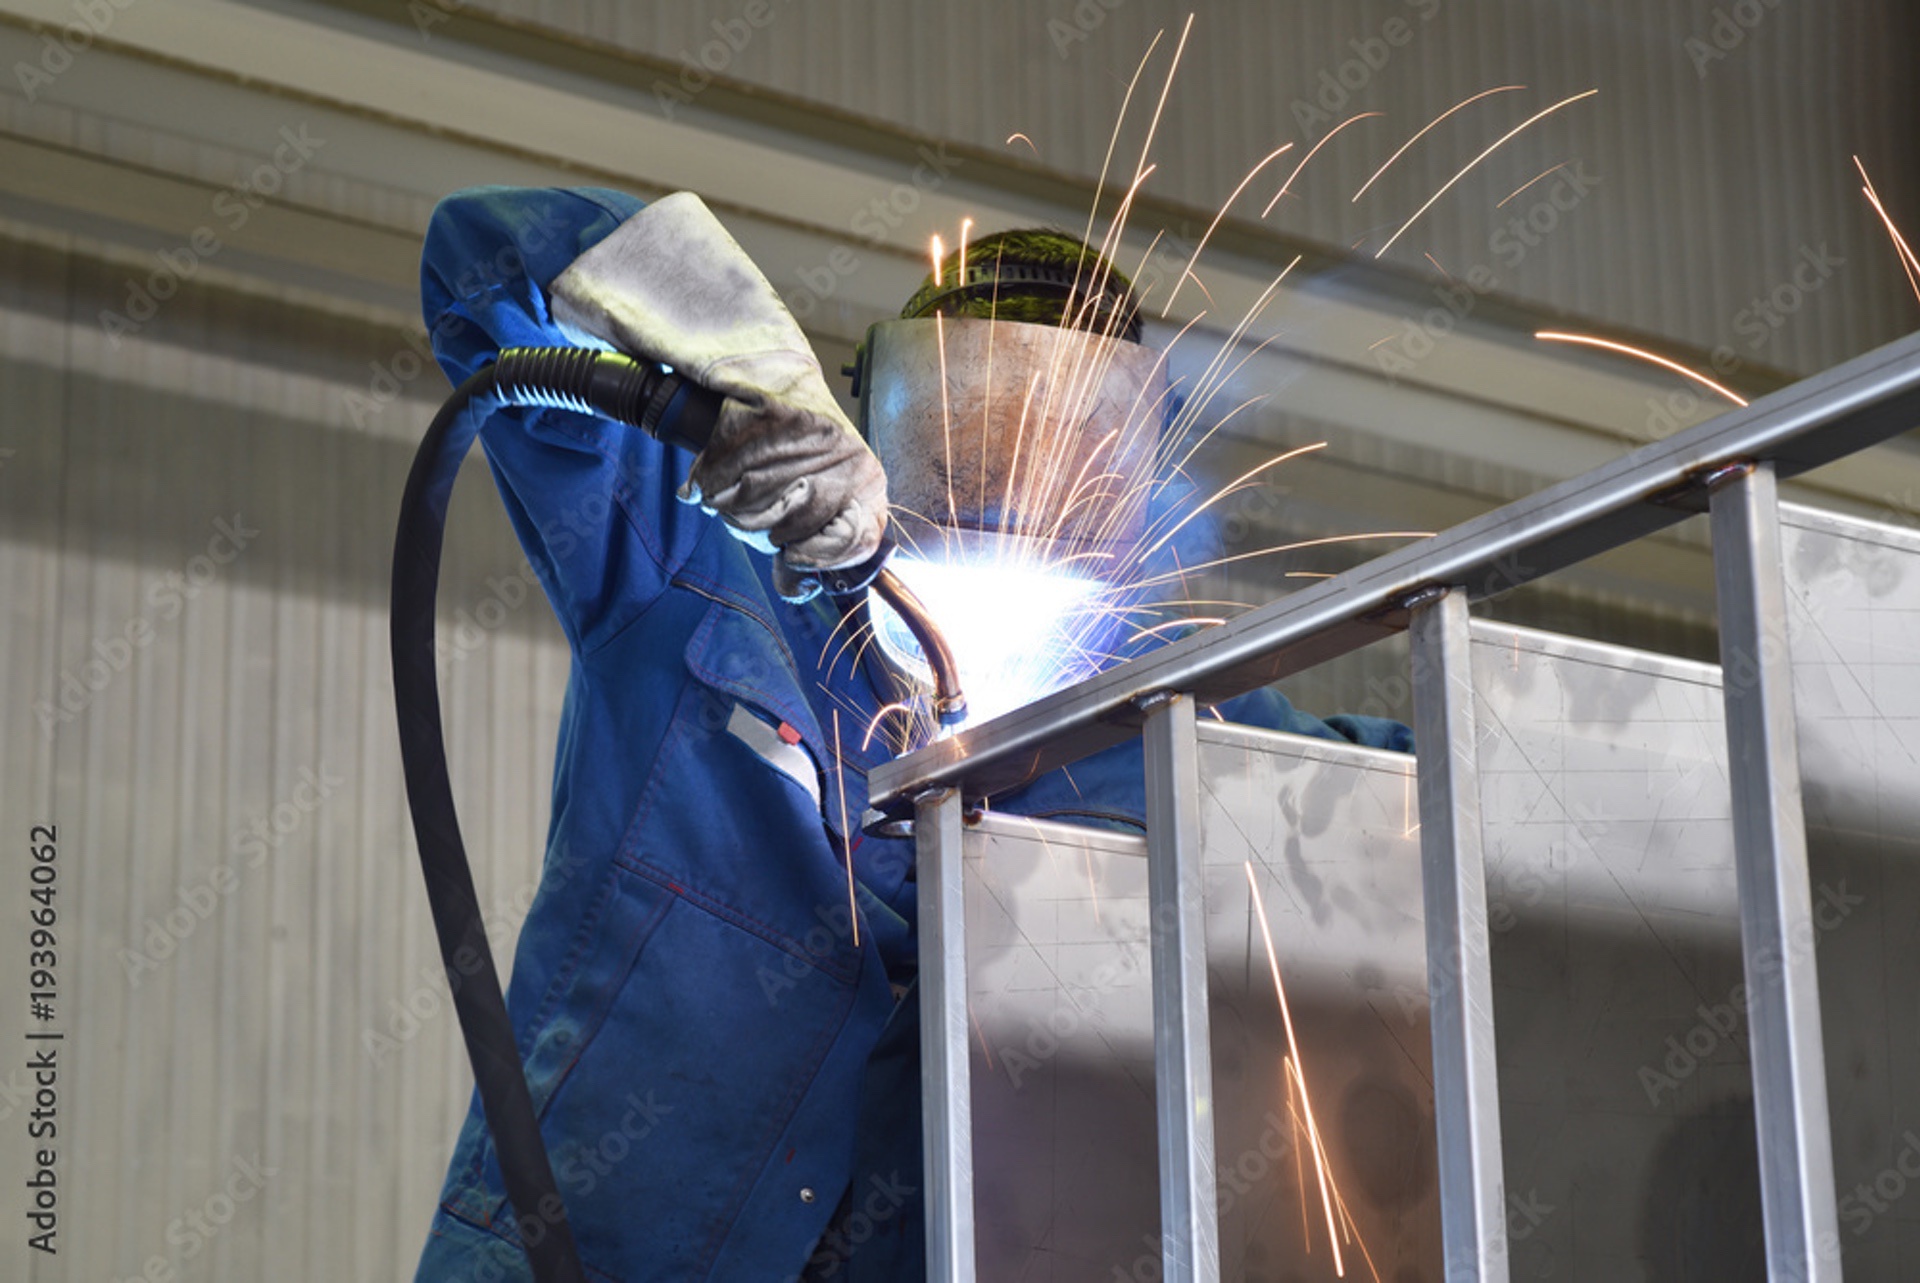
Welding stainless steel requires understanding both the welding process and the steel’s reaction to heat and mechanical stress. The weld must not only be structurally sound but also maintain essential properties like strength, toughness, and corrosion resistance.
A key concern with welding stainless steel, unlike carbon steel, is protecting its chromium content from oxidation to ensure it remains effective against corrosion and does not form oxides that could weaken the weld.
Key Considerations for Welding Stainless Steel Grades

| Austenitic | Ferritic | Martensitic | Duplex | PH Steels | |
|---|---|---|---|---|---|
| Thermal Expansion | High, causing residual stress | Low | Moderate | Moderate | Moderate |
| Shielding Gas Requirements | Inert gases with 3-5% nitrogen | Inert; stabilized ferritics avoid nitrogen exposure | Inert; very clean surfaces required | Inert with nitrogen to retain alloy composition | Inert, fully shielded |
| Preheating | Typically not required | Semi-ferritics require annealing to avoid martensite | 250-300°C for higher carbon content | Limited preheating; avoid high temperatures | Not required for general welding |
| Postweld Treatment | May need annealing for stress relief | Stabilized ferritics avoid martensite; minimal heat input | Final heat treatment required for designed properties | Solution annealing may restore phase balance | Required to homogenize structure |

Comparison of Welding Metals
Stainless Steel Welding Joints
Butt Welding
- A butt joint refers to two metal pieces located side by side for welding. A preliminary edge preparation is essential for a high quality welding outcome.
- The butt weld is relatively easier than the other joints and it withstands stress better than the others.
- It is the most common welding joint in fabricating structures.
Corner Welding
- Corner joints are very similar to Tee joints.
- The main difference is the location of the metal is positioned.
- In Tee joint, one metal is positioned in the center of the other, whereas in corner joints work pieces meet in the corner forming an ‘L’ shape.
Tee Welding
- Tee welding joints are created when two metal parts intersect at a 90° angle.
- This results in the edges getting together in the centre of a component in a ‘T’ shape.
- Tee joints are also a type of fillet weld.

Lap Welding
- Lap joint refers to a joint when one part laps onto the other one.
- The welding between the two parts is done by a fillet weld.
- The major shortcoming of the lap joint is that some area below the weld pool is prone to rust.
Edge Welding
- The edge welding joint is used to join parts that are parallel to each other.
- Edge joints are often used for sheet metal welding
- A cleaner and smoother weld surface than a butt joint.

Stainless Steel Welding Methods


Quality Control
Cost Drivers

Case Study 1 : When stainless steel parts no longer fit
A precision manufacturer came to us facing a massive bottleneck. They were rolling out a high-stakes batch of thin stainless steel equipment housings. Before welding, the parts fit like a glove—but as soon as the welds cooled down, thermal distortion pulled the assemblies completely out of square. Installing the equipment covers became a constant struggle, forcing technicians to manually straighten every single unit. They were losing valuable shop-floor hours, burning through labor costs, and watching their delivery schedule slip away.
The challenge
Our client didn’t just need a temporary band-aid; they needed a foolproof, repeatable welding process. Because different operators were using their own fixture setups and welding sequences, quality varied wildly from shift to shift. They needed a standardised method that controlled distortion while maintaining complete weld integrity.
A practical solution
That is where our team stepped in. We took a single trial assembly and engineered a custom, repeatable blueprint to eliminate distortion before full-scale production began:
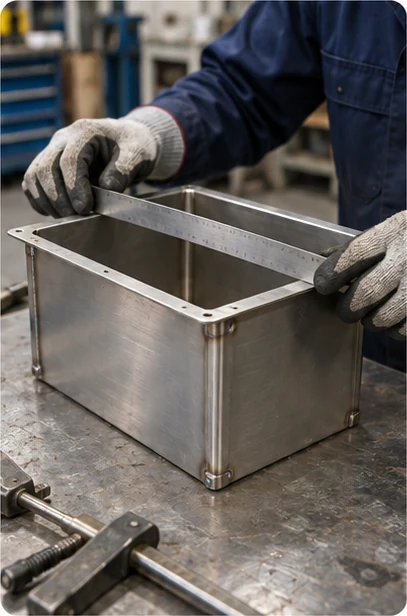
Checking housing flatness
What the client gained
By locking in a proven manufacturing method upfront, our client completely eliminated expensive post-weld rework. They turned an unpredictable manufacturing headache into a streamlined, high-yield production line—delivering perfectly square housings right on schedule, every single time.
Case Study 2: When a stainless steel weld repeatedly cracks
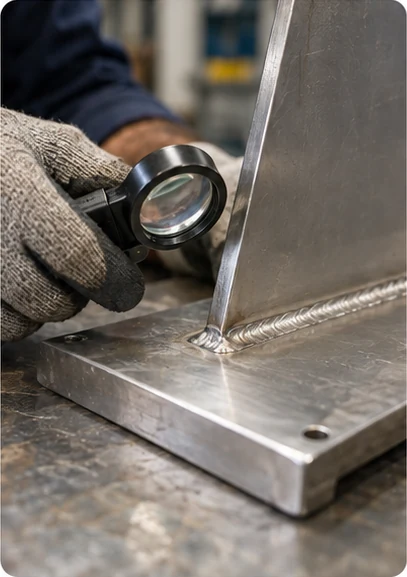
Visual Inspection of a welded connection
An industrial processing plant reached out to us with a critical problem: a high-stress welded attachment on their equipment kept cracking. Every time it broke, their maintenance team patched the crack, ground it down, and put the machine back to work. But like clockwork, the crack kept reappearing in the exact same location. The repeated downtime was draining their operational budget and putting production targets at risk.
The challenge
Quick patch jobs were failing because they merely reproduced the exact same structural flaw that caused the crack in the first place. Stopping chronic weld failure required a deep-dive investigation into joint design, mechanical loads, and the operating environment to fix the root cause once and for all.
A practical solution
We brought in our metallurgical and welding experts to perform a root-cause investigation and engineer a permanent, heavy-duty solution:
What the client gained
We helped our client break the cycle of costly, continuous repairs. By replacing temporary fixes with an engineered structural solution, the client eliminated unscheduled downtime, extended equipment life, and secured peace of mind for their entire operations team.
How can we help you ?
Stainless Steel Welding Services are indispensable to various industries and their success depends on the careful selection of contractors.
Novelty Structures stands out as a reliable partner in providing high-quality welding services tailored to demanding industrial needs.
FAQ
Absolutely! We specialize in custom welding and fabrication projects. Whether you need a unique design, prototype, or specialized repair, our experienced welders can help bring your vision to life.
Yes, all our welders are certified. We prioritize safety and quality in every project.
Yes, we offer finishing services such as grinding, polishing, and painting to ensure your project looks professional and is protected against rust and corrosion.
Yes, we have the expertise and equipment to handle large-scale industrial welding projects. Contact us to discuss your requirements, and we’ll provide a customized solution.
Yes, we provide structural welding services for buildings, bridges, and other infrastructure projects. Our team ensures that all welds meet the necessary structural integrity and safety standards.
We follow strict quality control procedures, including:
- Using certified materials and consumables
- Conducting thorough inspections before, during, and after welding
- Employing experienced, certified welders with advanced training
Yes, in addition to welding, we provide:
- Metal Cutting
- Bending and Forming
- Drilling and Machining
- Assembly and Finishing
Yes, we offer powder coating as optional finishing services to protect your project from corrosion and enhance its appearance.