
Novelty Structures Manufactures Contract Aluminium Fabrications for various Industrial Projects
- Why we need aluminium fabrications ?
- Why Aluminium is good for Fabrication ?
- Aluminium Fabrication Processes
- Fabrication of Different Aluminium Alloys
- Challanges in Aluminium Fabrication
- Case Study 1: Serial Aluminium Fabrication Quality
- Case Study 2: Design for Manufacturability (DFM) for Aluminium Fabrication
- Case Study 3: Custom Multi-Position Fixturing
- How can we help you ?
- FAQ
- Knowledge Hub

Applications
•Doors and Windows
•Decorative Panels
• Enclosures and Casings
• Storage Tanks
•Display Booths
•Temporary Structures
•Art Sculpture
•Signage & Barriers
•Solar & Wind Projects
•Oil & Gas & Offshore
• Process Equipment
• Machinery
•Cooling Towers
•Heat Exchangers

Why Aluminium is good for Fabrication ?
Aluminium Fabrication Processes


Case Study 1: Serial Aluminium Fabrication Quality
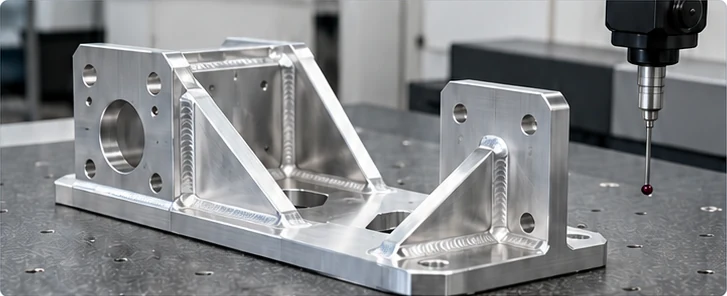
Aluminium assembly inspection
| Challenge | Solution | Impact |
|---|---|---|
| Ensuring 100% component fitment and functional alignment across high-volume repeat orders without batch-to-batch dimensional drift or thermal distortion. | Implementation of a 4-part production control framework, balanced welding sequences, and stage-gate functional inspection prior to final release. | Complete elimination of assembly line fitment delays, guaranteed process capability (Cpk), and full end-to-end traceability from approved drawing to final CMM report. |
Background & Project Challenge
In serial aluminium manufacturing, true quality is defined by whether components fit and function consistently throughout an entire production batch and across subsequent deliveries over time. While an approved initial sample establishes the baseline specification, maintaining consistent results across repeat deliveries requires a strictly documented and controlled manufacturing process.
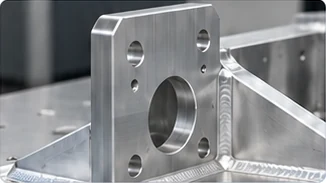
Mounting face and hole position detail
A premier OEM client required volume production of complex welded aluminium assemblies. In high-volume aluminium fabrication, key functional features—such as mounting faces, hole positions, mating clearances, and overall spatial alignment—are highly vulnerable to dimensional variance. Without systematic quality controls, common workshop risks such as thermal movement during welding, fixture spring back, unrecorded setup changes, and unmanaged drawing revisions can cause costly assembly line downtime.
Engineering Strategy & Quality Control Framework
To resolve these serial manufacturing challenges, Novelty Structures implemented a comprehensive four-stage quality assurance protocol linking engineering drawings directly to workshop manufacturing processes and stage-gate inspection checks.
Identifying Critical Functional Features: Prior to production, engineering teams identify features essential to final assembly—specifically mounting faces, hole positions, mating clearances, and overall spatial alignment. Intermittent inspection of these features during early manufacturing stages enables early defect detection before secondary operations add unnecessary cost.
Fixturing & Thermal Distortion Control: For welded aluminium assemblies, controlling heat-induced movement is critical. Using accurate rigid fixtures combined with a balanced, symmetrical welding sequence mitigates thermal distortion. While physical restraint prevents movement during welding, industry fabrication standards note that tight restraint can introduce internal residual stresses. Therefore, final dimensional verification is always performed in a free-state condition after parts are released from the welding fixture to ensure true geometric compliance.
Serial Production Control Framework
To guarantee repeatability across repeat orders, the manufacturing execution plan addresses four fundamental production control questions:
| Production Question | Manufacturing Control Established | Engineering & SEO Significance |
|---|---|---|
| What defines an acceptable component? | Approved drawing revision with clearly identified functional dimensions and explicit tolerance limits. | Guarantees clear tolerance bounds for mounting interface surfaces and hole pattern alignments. |
| How is the batch released for manufacture? | Mandatory first-piece inspection and approval against agreed requirements prior to full run. | Prevents systemic machine setup errors from multiplying across entire production runs. |
| How is consistency maintained? | Recorded machine setups, in-process stage checks, and defined intervention thresholds when dimensions drift. | Maintains process capability (Cpk) and enables immediate containment before out-of-spec parts are built. |
| How is the result reproduced next time? | Retained manufacturing instructions (SOPs), revision control logs, and identifiable production batch codes. | Secures perfect repeatability for future re-orders regardless of operator or equipment scheduling. |
Closed-Loop Defect Management
When a dimensional defect occurs, rectifying the individual component is only the first step. The quality protocol executes a closed-loop containment workflow:
For purchasing teams and quality managers, the most reliable evidence of manufacturing capability is a clear, documented connection between drawing revisions, manufacturing methods, and stage-by-stage inspection results—providing far greater confidence than a basic final inspection stamp.
Case Study 2: Design for Manufacturability (DFM) for Aluminium Fabrication
| Challenge | Solution | Impact |
|---|---|---|
| Manufacturing a large, complex 5754 aluminium panel as a continuous piece without encountering press-brake frame collisions. | Design for Manufacturability (DFM) optimization replacing an un-bendable single piece with an approved laser-cut, formed, TIG, and laser-welded hybrid assembly. | Total elimination of machine collision risk, perfect geometric precision, zero part deformation, and streamlined serial supply. |
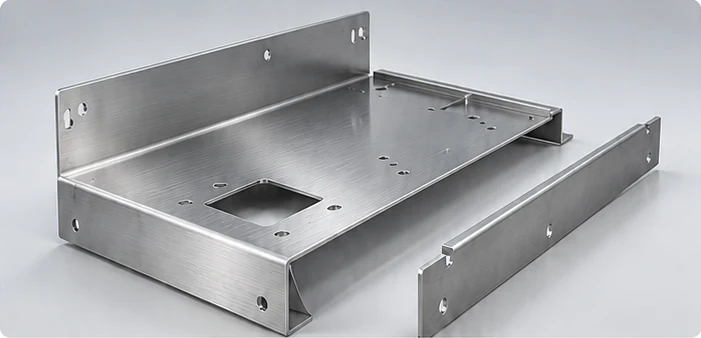
Formed aluminium panel
Project Challenge & Tool Access Constraints
A Novelty Structures’ client requested the fabrication of a custom 5754 aluminium panel engineered as a single, unsegmented continuous component. While single-piece panel designs appear straightforward on engineering drawings and minimise component counts, they can create insurmountable manufacturing obstacles during forming operations in the workshop.
During the pre-production manufacturing review, collision modelling identified a critical physical constraint: during the proposed press-brake bending sequence, the panel’s complex return geometry would collide directly with the press-brake machine frame. Forcing the bend would cause severe part deformation, damage expensive tooling, and result in unacceptable scrap rates.
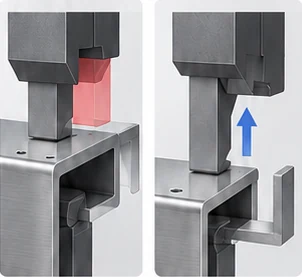
Tool access
DFM Optimization & Hybrid Manufacturing Strategy
The essential commercial lesson from this project is that part count alone does not determine manufacturing efficiency. A design with fewer individual pieces may still require difficult handling or a physically impossible forming sequence.
Rather than compromising part tolerances or risking workshop delays, the engineering team conducted a comprehensive Design for Manufacturability (DFM) review and proposed an approved hybrid manufacturing methodology:
Manufacturing Methodology Comparison
Evaluating the unsegmented concept against the optimised DFM hybrid workflow demonstrates clear advantages in process control and part quality:
| Manufacturing Approach | Tool Access & Geometry | Process Risk Profile | Production & SEO Impact |
|---|---|---|---|
| Un-Segmented One-Piece Design | Collides directly with press-brake frame during secondary flange bends. | Severe risk of part deformation, frame collision, high scrap rates, and lost alignment. | Impractical for repeat serial production; requires slow, manual workshop adjustments. |
| DFM Hybrid Assembly (Laser + Form + Weld) | 100% unobstructed machine access across cutting, bending, and welding cycles. | Zero collision risk; tight control over thermal distortion via precision laser welding. | High repeatability, fast cycle times, exceptional structural integrity, and perfect cosmetic finish. |
Pre-Release Resolution for Repeat Supply
To ensure smooth repeat production, these manufacturing constraints were completely resolved before releasing the production batch. The client defined the essential interface surfaces, cosmetic requirements, and allowable joint locations, while the engineering team established a feasible, standardised production sequence. This proactive DFM process prevented a design constraint from becoming a recurring workshop adjustment.
Case Study 3: Custom Multi-Position Fixturing
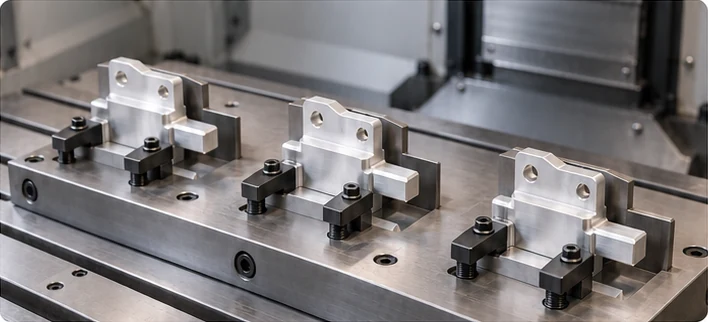
Three-position aluminium fixture.
| Challenge | Solution | Impact |
|---|---|---|
| High repetitive handling labor and tool obstruction when CNC machining a 28-piece batch of small, irregular aluminium parts with projecting side connections. | Engineering a custom multi-position fixture holding three components simultaneously while providing generous relief around projecting features. | Substantial reduction in manual setup handling, unrestricted multi-axis tool access, and exceptional position-to-position dimensional consistency across all 28 parts. |
Project Challenge & Production Bottlenecks
In a documented 28-piece precision aluminium machining order, the production team faced a severe handling obstacle: the component was small, irregular in shape, and featured a prominent projecting side connection.
Standard vice clamping was impossible without obstructing cutting tool access to the projecting feature. Furthermore, loading, aligning, and probing each of the 28 components individually would add massive non-cutting handling time to every machine load cycle, drastically inflating unit production costs and extending delivery timelines.
Engineering Strategy & Custom Fixture Design
To address these handling bottlenecks and tool access constraints, Novelty Structures designed and manufactured a custom multi-position machining fixture tailored specifically to the part’s complex geometry.
Quality Verification & Process Control
To guarantee dimensional accuracy across all fixture locations prior to full batch execution:
Multi-Position Fixture Performance Analysis
A direct comparison between conventional single-part clamping and the custom dedicated fixture highlights substantial productivity gains:
| Operational Parameter | Standard Single-Part Clamping | Custom 3-Position Fixture Solution | Performance & Productivity Gain |
|---|---|---|---|
| Parts Clamped Per Setup | 1 Part per load cycle | 3 Parts per load cycle | 200% increase in fixture density per machine table load |
| Handling Overhead | High (28 individual part setups) | Low (10 setup cycles total) | Dramatic reduction in repetitive loading and manual alignment time (from 28 setups to 10) |
| Tool Access to Side Connection | Obstructed by standard vice jaws | Unrestricted clearance via engineered relief pockets | Full cutting tool access at maximum feed rates and spindle speeds |
| Dimensional Repeatability | Variable (Operator setup dependent) | Highly Consistent (Fixed reference datums) | Uniform accuracy across all 28 parts with zero position drift |
Conclusion for Recurring Supply
The key takeaway for recurring aluminium component orders is that overall productivity depends just as much on loading, positioning, and stage checking as it does on cutting speeds. Custom dedicated fixturing transforms repetitive machining tasks into efficient, predictable production runs when batch quantities and component geometries justify the initial tooling setup.
How can we help you ?
Aluminium Fabrications are indispensable to industrial projects and their success depends on the careful selection of contractors
Novelty Structures manufactures high-quality aluminium fabrications tailored to demanding industrial needs.
FAQ
Aluminium fabrication is the process of shaping, forming, and assembling raw aluminium into finished components or products. It involves various techniques such as cutting, bending, welding, machining, and surface finishing to meet specific design requirements.
- 1xxx Series: Pure aluminium (99 %+), excellent corrosion resistance, but low strength. Used for chemical tanks and electrical applications.
- 2xxx Series: Aluminium-copper alloys, high strength, but less corrosion resistant. Common in aerospace.
- 5xxx Series: Aluminium-magnesium alloys, excellent corrosion resistance and weldability. Common in marine and automotive.
- 6xxx Series: Aluminium-magnesium-silicon alloys, good balance of strength, corrosion resistance, and machinability. Widely used in construction.
- 7xxx Series: Aluminium-zinc alloys, very high strength, used in aerospace and defence.
Quality control ensures that fabricated components meet the required specifications and tolerances. Key steps include:
- Dimensional Checks: Using calipers, micrometers, and coordinate measuring machines (CMM).
- Weld Inspections: Non-destructive testing (NDT) methods like X-rays or ultrasonic testing to detect defects.
- Surface Finish Checks: Ensuring consistent finishes, thickness of coatings, or anodizing layers.
Material Testing: Verifying properties like tensile strength and hardness using standardized tests (e.g., ASTM standards).
Surface defects can arise during handling, machining, or finishing.
| Defect | Cause | Solution |
| Scratches and Dents | Poor handling or inadequate protective measures. | Use protective films during transport and fabrication. |
| Porosity | Incomplete removal of oxides or contaminants during welding. | Clean thoroughly before welding and ensure proper shielding gas coverage. |
| Discoloration or Staining | Improper cleaning, exposure to moisture, or contamination. | Use anodizing or powder coating, and store aluminium in a dry, controlled environment. |
| Oxidation | Natural reaction of aluminium with air to form oxide layers. | While this is natural, it can be controlled with surface treatments like anodizing or painting. |
Aluminium’s high thermal conductivity can lead to distortion due to uneven heating.
Preventive Measures:
- Preheating: Reduces thermal gradients, especially for thicker sections.
- Clamping and Fixtures: Holds parts rigidly in place to minimize warping.
- Controlled Welding Speed: Adjusting travel speed and heat input to avoid excessive temperatures.
- Weld Sequencing: Alternating weld locations to balance stresses.
Knowledge Hub