
Experienced Stainless Steel Fabricator for Contract Fabrication

Why Stainless Steel Matters
Applications of Stainless Steel
Tanks and components for sewage and wastewater treatment.
Military and defense equipment needing high durability.
Jewelry, watches, and personal accessories.
Reactors and processing equipment for corrosive environments.
Oil and gas pipelines and offshore platforms.
Heat exchangers and boilers.
Hospital furniture and equipment (beds, trolleys, and sterilizers).
Hygienic surfaces in labs and pharmaceutical facilities.
Decorative elements and modern interiors.
Kitchen appliances, cutlery, and cookware.
Brewery and dairy equipment.


Duplex Stainless Steels
Duplex stainless steels are highly corrosion-resistant and work-hardenable alloys. They typically contain elevated levels of chromium, ranging from 18% to 28%, and lower to moderate amounts of nickel, varying between 1.5% and 8%. The remarkable corrosion resistance and superior mechanical properties of duplex stainless steels stem from their chemical composition and balanced microstructure, which comprises approximately equal volume percentages of ferrite and austenite. This duplex nature imbues duplex stainless steels with properties characteristic of both austenitic and ferritic stainless steels.
Due to their duplex structure, duplex stainless steels are generally tougher than ferritic stainless steels. In some instances, the strength of duplex stainless steels can be double that of austenitic stainless steels.

Advantages of Duplex Steels
Applications of Duplex Steels


Fabrication of Duplex Steels
Welding Duplex Steels

Quality Control in Stainless Steel Fabrication
Stainless Steel Finishes
A- Mechanical Finishes


Comparison of Mechanical Finishes
B- Chemical Finishes


Comparison of Chemical Finishes


Stainless Steel Fabrication Case Studies
Practical Project Lessons, Causes and Workshop Improvements at Novelty Structures
Case Study 1: The Rust Mystery on 'Clean' Stainless Equipment
Background
During a facility equipment upgrade, a batch of new stainless steel components supplied by Novelty Structures developed noticeable brown rust spots shortly after exposure to moisture. The material certificates confirmed that the parts were made from the specified high-grade stainless steel, ruling out the supply of an incorrect material.
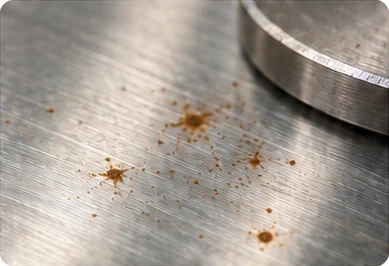
Stainless steel surface contamination
Incident & Root Cause Analysis
Our investigation into workshop practices identified two sources of contamination:
Corrective Action Plan
| Problem Area | Root Cause | Implemented Solution |
|---|---|---|
| Tooling Control | Grinding discs and wire brushes had been shared between metals. | We introduced dedicated, colour-coded abrasives reserved for stainless steel work. |
| Shop Layout & Storage | Finished parts had been stored near carbon steel grinding areas. | We created separate stainless steel storage areas away from sparks and required protective covers. |
| Quality Control | Rust spots had been polished away without checking the cause. | We required checks after handling and confirmed whether marks came from contamination or corrosion of the stainless steel before treatment. |
Case Study 2: The Mismatched Equipment Covers
Background
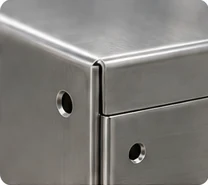
An equipment manufacturer wanted to eliminate recurring paint maintenance and corrosion problems in a harsh operating environment by replacing painted mild-steel enclosure covers with 304 stainless steel. At Novelty Structures, we reused the existing laser-cutting drawings for the flat sheets and the programmed bending machine settings. However, during trial assembly, the folded edges did not line up with the adjoining parts.
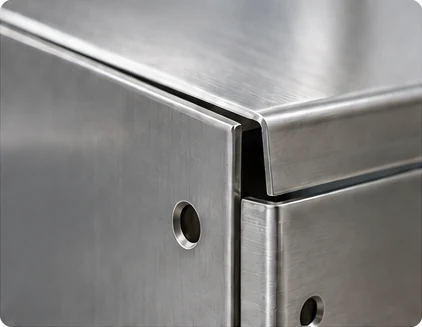
Equipment cover fit
The Technical Challenge
The trial showed why we needed to account for the different ways stainless steel and mild steel behave during bending:
Implementation Protocol
To correct the fit, we introduced a four-step process to check and adjust the setup:
STEP 1
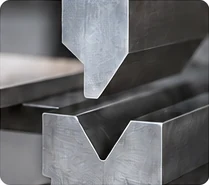
Tooling Trial
(Test grade & thickness)
STEP 2
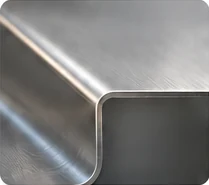
Geometry Audit
(Measure angle & radius)
STEP 3
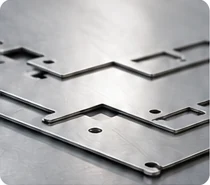
Pattern Adjustment
(Recalculate flat blank)
STEP 4
Trial Fit-Up
(Verify full assembly)
Case Study 3: The Warped Washdown Panels
Background
For a food production facility, Novelty Structures upgraded washdown panels from painted carbon steel to 304 stainless steel to improve hygiene and corrosion resistance. The panels included welded stiffeners and mounting brackets. We used the established welding sequence developed for carbon steel. After welding, however, the stainless steel panels had bowed and distorted badly, preventing them from sitting flat when mounted.
Technical Breakdown
Response to Heat: Austenitic stainless steels, including 304, expand around 50% more than carbon steel for the same temperature rise and conduct heat away more slowly.
Why the Panels Warped: Heat stayed near the welds for longer, causing those areas to expand and then shrink as they cooled. This pulled the panels out of shape.
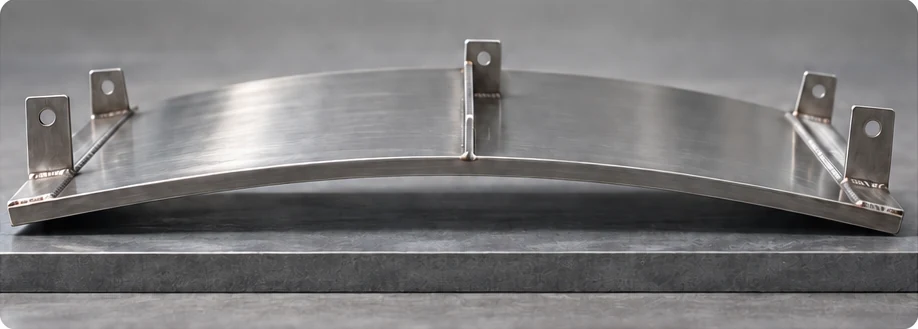
Washdown panel distortion
Standard Operating Procedure (SOP) & Preventive Controls
Case Study 4: Overcoming Specification Ambiguity to Cut Rework Costs
Background
On custom stainless steel fabrication orders at Novelty Structures, unclear requirements had led to budget overruns, disagreements and delayed deliveries. Expensive cosmetic polishing had been applied across entire components, including hidden structural areas. Meanwhile, thin, flexible panels had passed workshop inspection but failed to fit during installation on site.
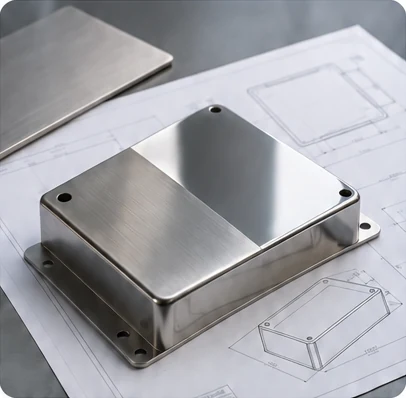
Surface finish and inspection
Standardised 5-Point Fabrication Protocol
We introduced five clear specification requirements for all future procurement drawings:
| Specification Rule | Common Pitfall | Standardized Requirement |
|---|---|---|
| 1. Surface Zoning | Applying a high polish to hidden structural parts. | We marked visible, product-contact and hidden surfaces clearly on drawings. |
| 2. Finish Criteria | Using vague terms such as ‘polished’ or ‘cleaned’. | We specified surface roughness (Ra), passivation treatment after fabrication to support corrosion resistance, and inspection methods. |
| 3. Pre-Assembly Access | Being unable to weld or clean internal joints after assembly. | We checked access before closing assemblies and agreed checks at intermediate stages. |
| 4. Restrained vs. Free | Measuring flexible parts while clamped in holding fixtures. | We defined whether dimensions applied to free-standing parts or parts held in the specified installed position. |
| 5. Reference Sample | Inconsistent quality across repeat orders. | We kept the first approved unit (‘golden sample’) with its drawing revision, finish records and material certificates. |
How can we help you ?
Stainless steel fabrication is widely used across various industries and its success depends on the careful selection of a stainless steel fabricator.
Novelty Structures provides high-quality stainless steel fabrication services tailored to demanding industrial needs.
FAQ
Stainless steel fabrication refers to the process of creating stainless steel structures, components, or products by cutting, bending, welding, and assembling various pieces of stainless steel material. It’s commonly used in industries like construction, food processing, aerospace, and automotive due to stainless steel’s durability, corrosion resistance, and aesthetic appeal.
- Corrosion Resistance: Stainless steel is much more resistant to rust, corrosion, and staining compared to other metals like carbon steel or aluminum.
- Non-reactive: It doesn’t react with food, beverages, or chemicals, making it perfect for medical, food, and beverage industries.
- Long-lasting: Its durability ensures it lasts longer without the need for frequent replacement or repairs.
- MIG (Metal Inert Gas) welding: Faster and easier to learn, MIG welding is commonly used for thicker pieces of stainless steel and high-production environments. It requires a continuous wire feed and uses a shielding gas.
- TIG (Tungsten Inert Gas) welding: Provides more precise and cleaner welds, making it ideal for thinner stainless steel. It requires more skill but offers superior control, especially for intricate or high-quality applications.
Yes, while stainless steel is often used for its natural appearance, it can be painted or coated for additional protection or aesthetic purposes. Common coatings include:
- Powder Coating: Adds color and enhances durability.
- PVD (Physical Vapor Deposition): Adds decorative colors like gold, black, or bronze while retaining stainless steel’s durability.
- Epoxy Coatings: Used in harsh environments for additional corrosion protection.
It depends on the type of stainless steel:
- Austenitic stainless steels (e.g., 304 and 316): Typically non-magnetic in their annealed state but can become slightly magnetic after cold working.
- Ferritic and Martensitic stainless steels (e.g., 430 and 410): Magnetic due to their higher iron content and crystalline structure.
Some challenges include:
- Work Hardening: Stainless steel tends to harden when worked, which can make cutting and forming more difficult.
- Thermal Expansion: It has a high rate of thermal expansion, which must be managed during welding to prevent warping.
- Corrosion during Fabrication: Improper handling, such as using contaminated tools, can introduce rust or surface damage.
- Precision Welding: Welding stainless steel requires precise temperature control to avoid overheating, discoloration, or weakening.
- Corrosion Resistance: Stainless steel is generally more corrosion-resistant than aluminum.
- Strength: Stainless steel is stronger and more durable but also heavier.
- Weight: Aluminum is lighter, making it ideal for applications where weight is a concern.
- Cost: Aluminum is typically less expensive but may require more maintenance over time.
- Applications: Aluminum is commonly used in lightweight structures, while stainless steel is preferred for strength, durability, and hygienic requirements.
- Cold-Rolled Stainless Steel: Rolled at room temperature, it has a smooth surface, precise dimensions, and increased strength. It’s used for applications requiring tight tolerances and a polished finish.
- Hot-Rolled Stainless Steel: Rolled at high temperatures, it’s easier to form and is more cost-effective, but it has a rougher surface and less precision. It’s often used for structural or heavy-duty applications.
To prevent warping:
- Proper Welding Techniques: Use controlled heat input and alternate welds on opposite sides.
- Clamping: Secure the stainless steel firmly during welding or cutting.
- Cooling: Allow the material to cool naturally or apply controlled cooling methods.
- Stress Relief Treatments: After fabrication, stress-relieving processes can help minimize residual stress.

Knowledge Hub