Steel sheet metal bending

Novelty Steel provides a comprehensive set of steel bending services for various industries and applications.

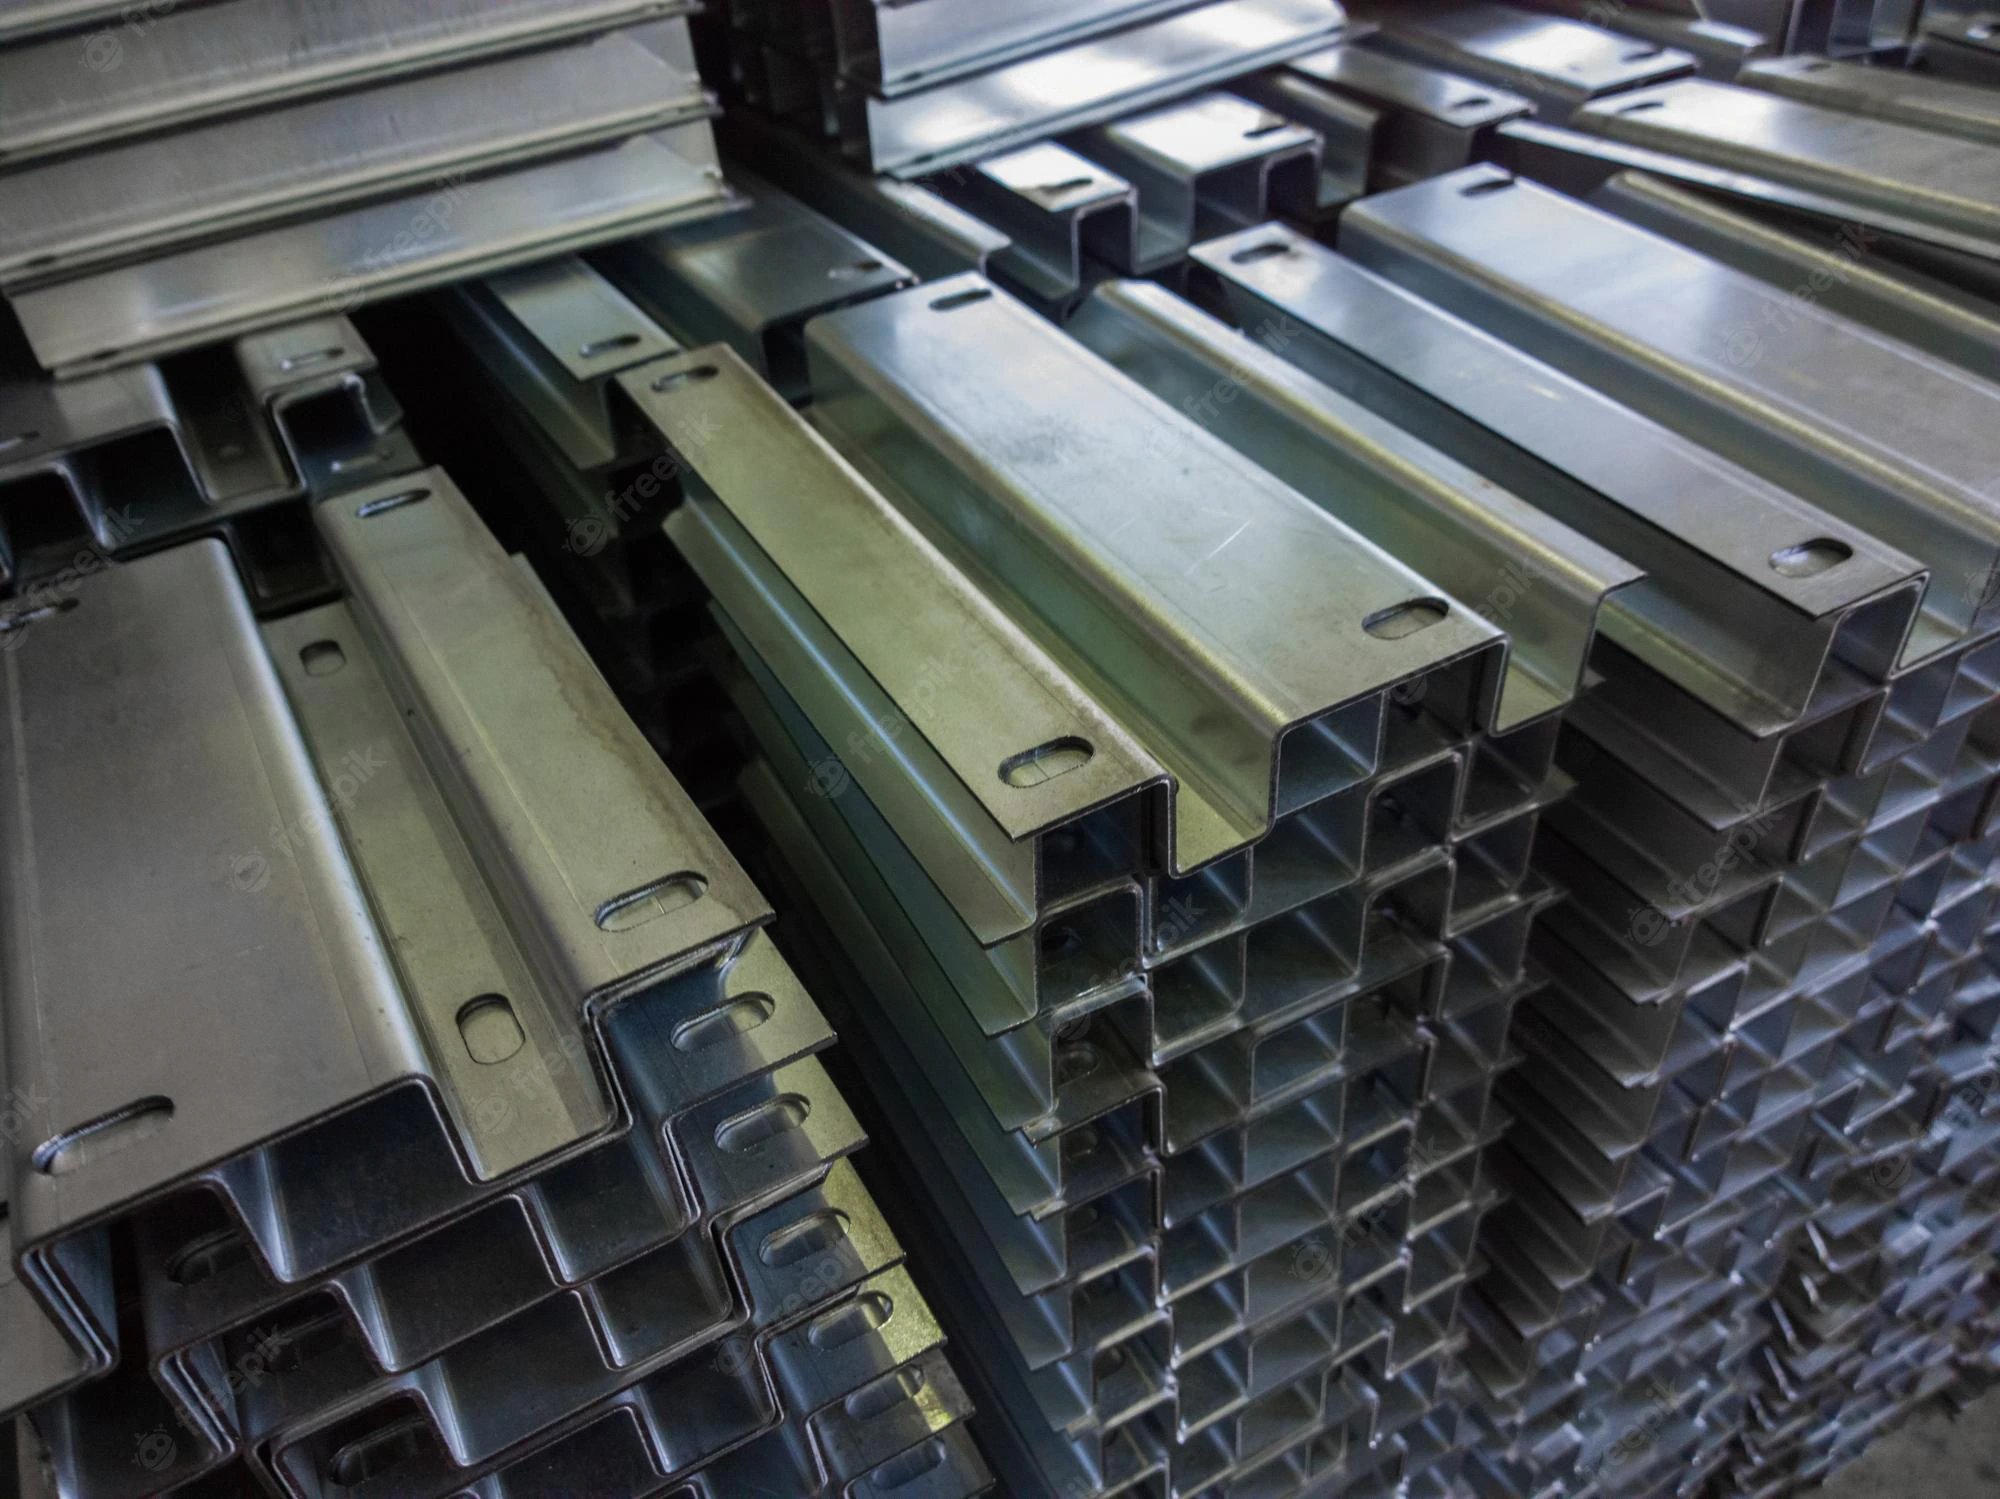
Sheet Metal Bending


Sheet metal bending involves shaping thin sheets of steel into desired forms by applying force. We use press brakes in various length and capacity to create complex angles and curves.

Sheet Metal Bending Part

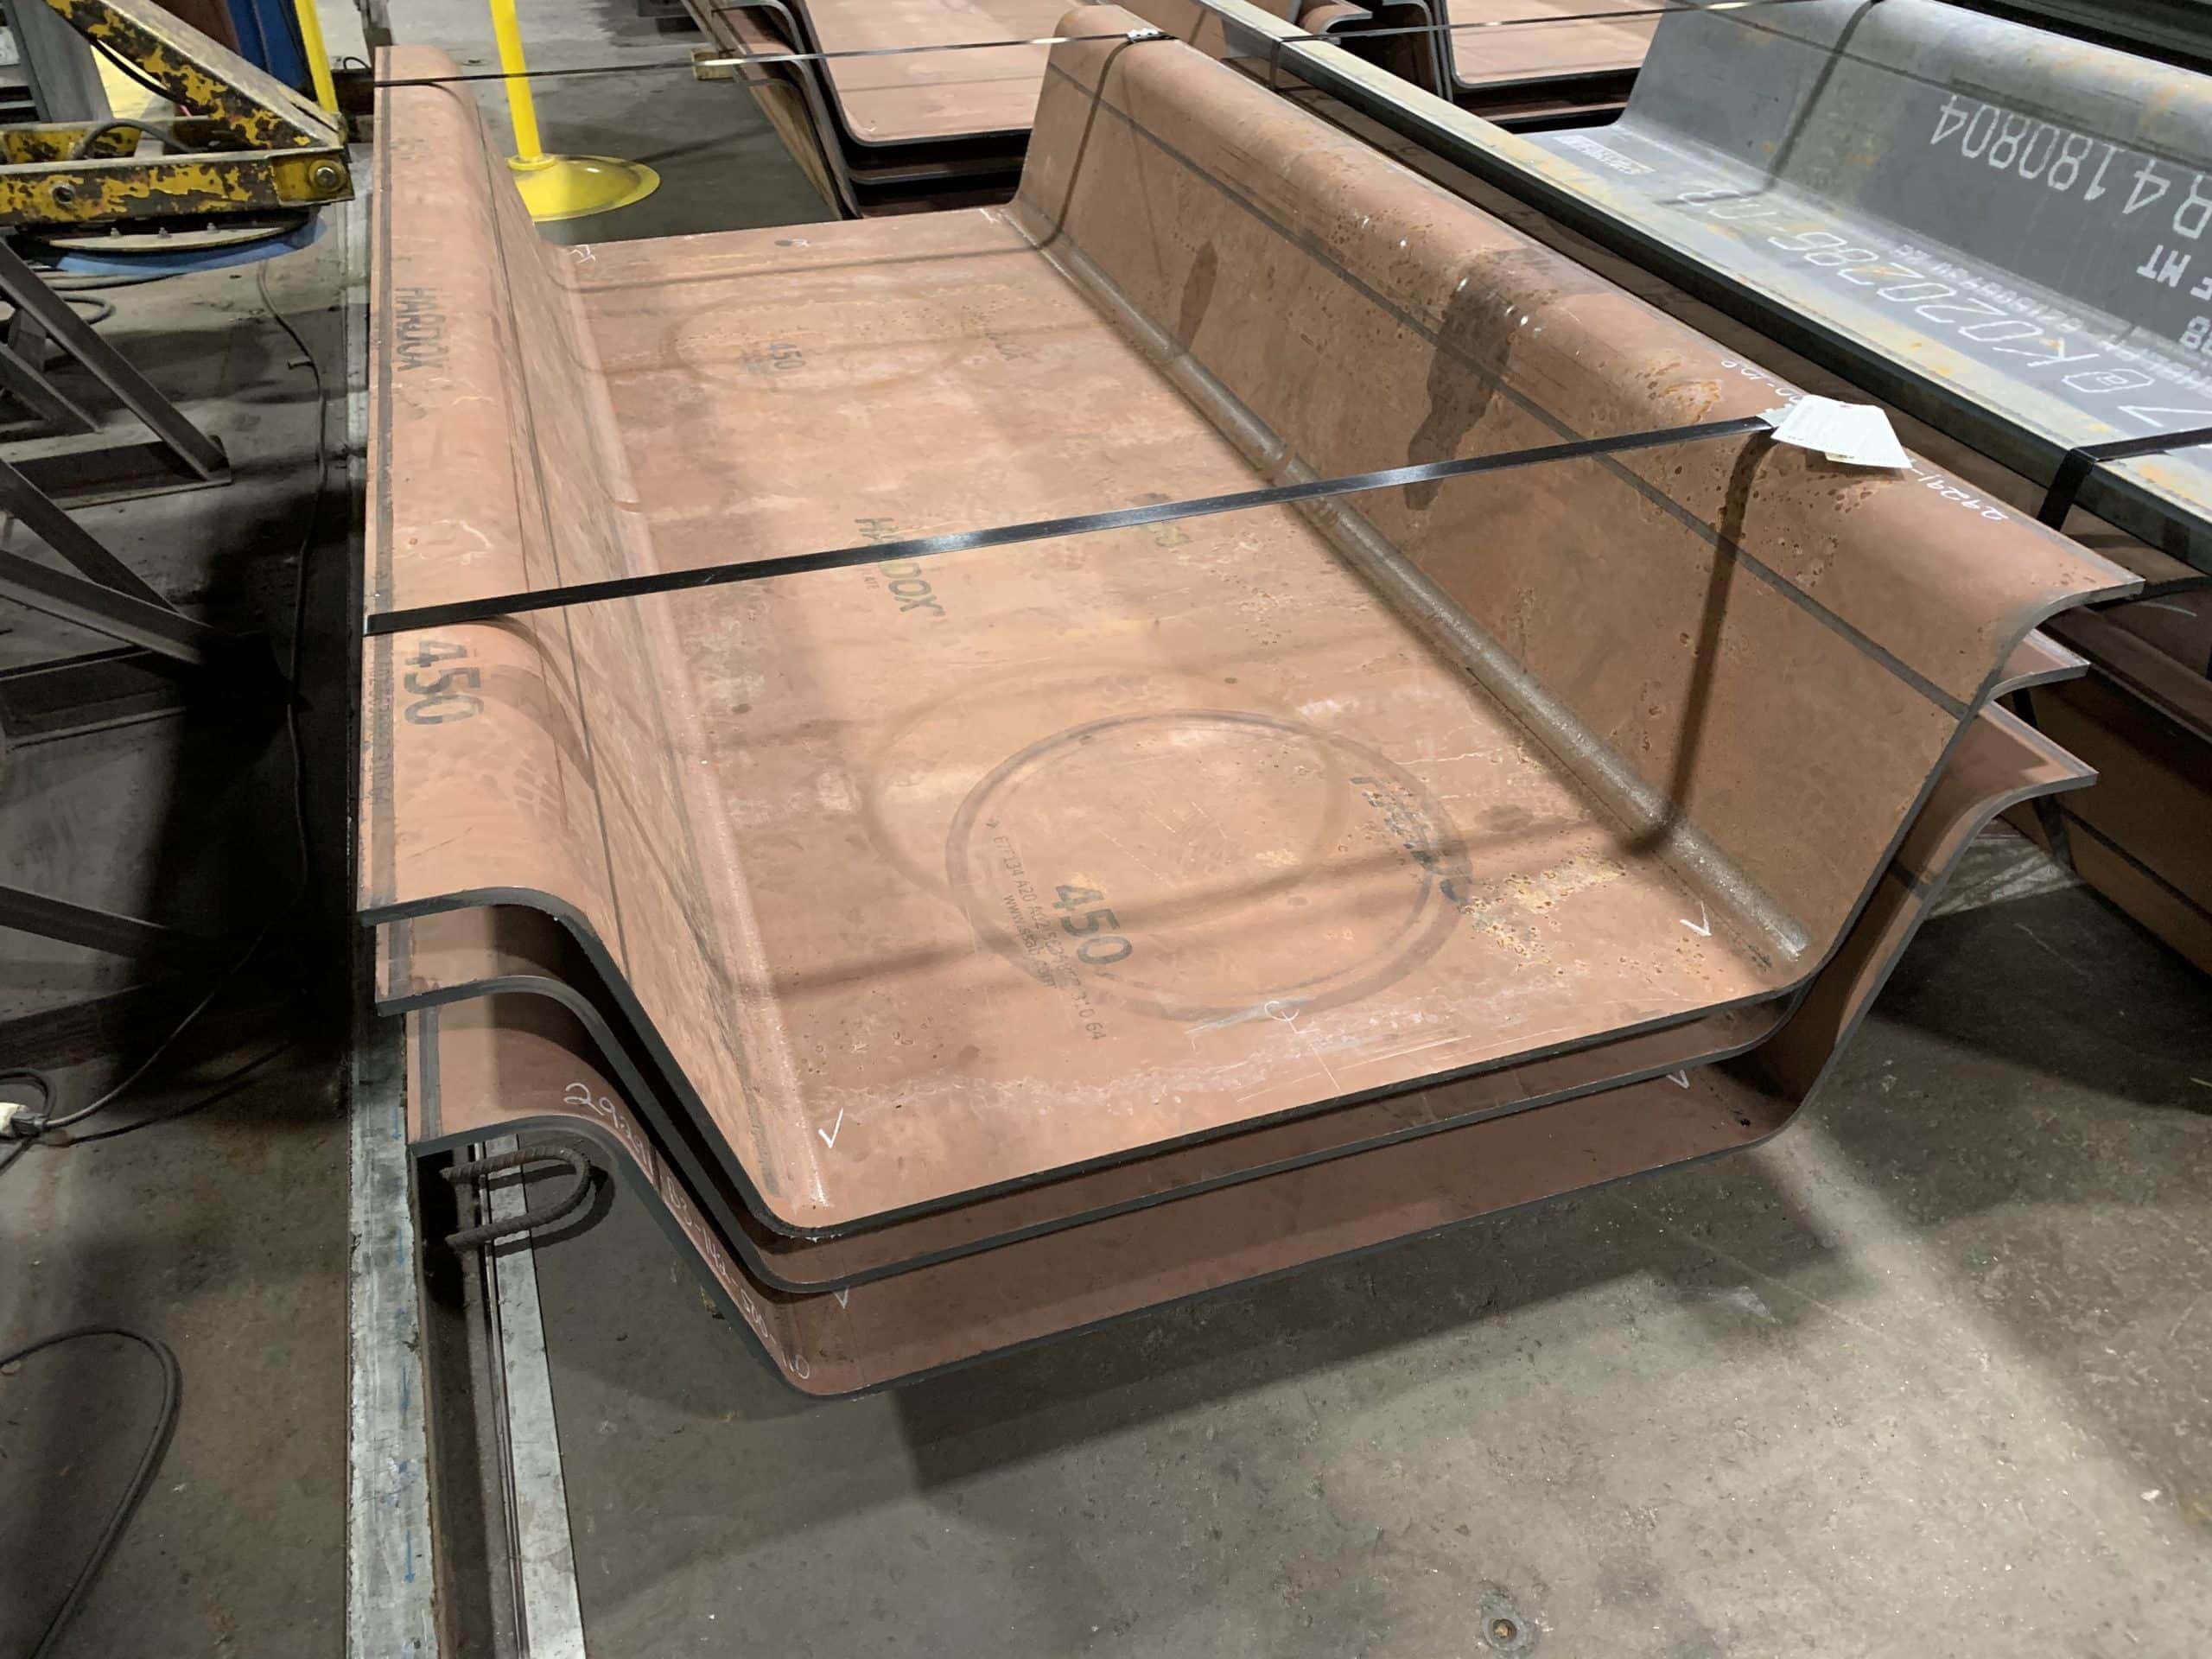
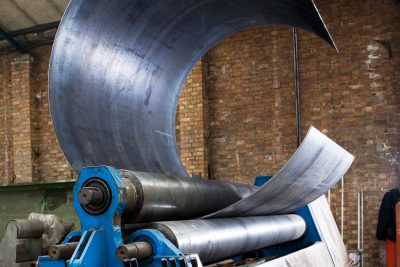
Plate Rolling

Plate rolling is a specialized bending process used to curve or roll thick steel plates into cylindrical or conical shapes. This process is essential for creating large industrial components such as steel silos, steel tanks and etc.

Applications


  • Storage tanks
  • Structural pipes and columns
  • Marine and shipbuilding parts

Benefits


  • Ability to handle heavy-duty steel plates
  • Accurate shaping of large, curved structures
  • Uniform Curve formation

Tube / Pipe Bending

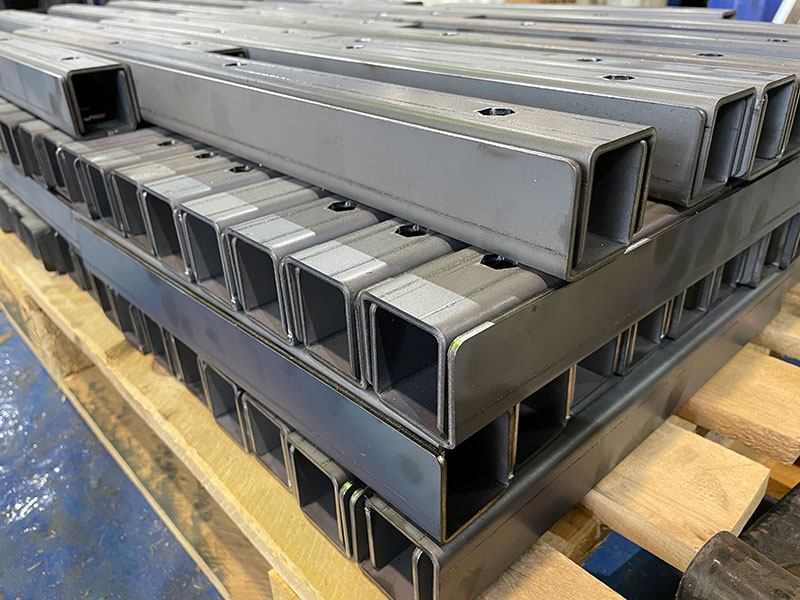
Steel tube and pipe bending involves bending hollow tubes or pipes into specific shapes without compromising their structural integrity. Various methods, including rotary draw bending and mandrel bending, are used for precision.

Applications


  • Handrails and safety barriers
  • Hydraulic systems
  • Furniture frames

Benefits


  • Maintains tube strength during bending
  • Versatile for different radius and angles
  • Customizable for various industries,

Steel Section Bending

Section bending refers to bending structural steel sections like beams, channels, or angles. This process is vital for creating curved elements in construction and infrastructure projects.

Applications


  • Arched beams for bridges and buildings
  • Curved staircases and railings

  • Custom structural components

Benefits


  • Handles a wide variety of profiles and shapes
  • Suitable for large-scale steel construction projects
  • Achieves smooth, consistent curves with minimal distortion

Metal Stamping

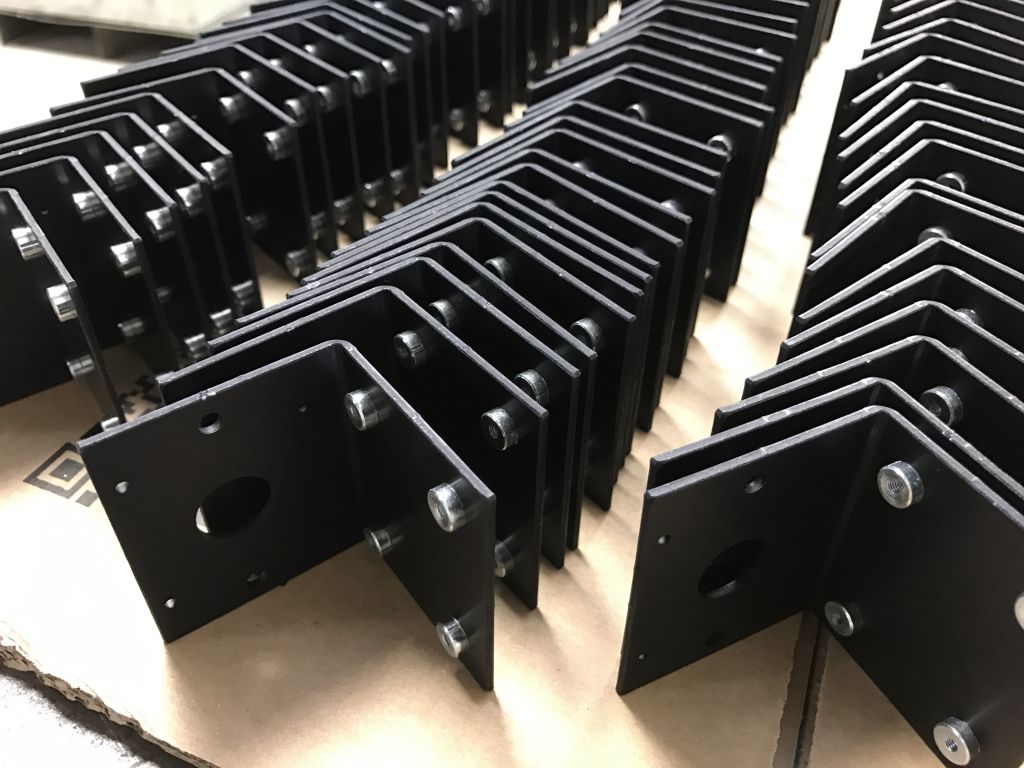
Stamping is a metalworking process where steel sheets are formed into desired shapes using a die and a press machine. This method is often used for high-volume production.

Applications


  • Automotive components (e.g., panels, brackets)
  • Electrical parts
  • Home appliances
  • Machine parts

Benefits


  • High-speed production for large quantities
  • Precision and uniformity in each piece
  • Cost-effective for mass production

Deep Drawing

Deep drawing is a metal forming process where a flat steel sheet is stretched into a deep, three-dimensional shape using a die. This technique is widely used for manufacturing seamless and hollow products.

Applications


  • Kitchen sinks
  • Car fuel tanks
  • Medical equipment

Benefits


  • Produces seamless, durable parts
  • Reduces material waste
  • Ideal for producing complex, deep shapes

Overcoming Steel Bending Challenges

Start with Consistent Raw Material

For repeat production, use the same specified material grade, thickness and delivery condition. Where practical, source material from the same heat number and retain plate or coil identification through processing.

A common heat number helps control material variation, but does not guarantee identical bending behaviour. Check actual thickness, review the material certificates and validate the setup when the material batch changes. Consistent strength and thickness help make spring back more predictable.

Press Brake Bending: Control Angle Variation

The challenge: Parts open to different angles after bending, or a long bend measures correctly at the ends but differently in the centre.

  • Establish spring back compensation using a trial part from the production material, measured after the bending load is released.
  • Keep the tooling, blank orientation and material specification consistent once the setup is approved.
  • Measure long bends at both ends and the centre. If the angle varies along the length, check tool alignment and crowning—the adjustment that compensates for machine deflection.

A correct reading at one position should not be used to approve the entire bend.

Plate Rolling: Reduce Flat Ends and Uneven Curvature

The challenge: A rolled shell has flat areas near the joint, or its edges do not meet with the required curvature.

  • Plan how both plate ends will be pre-bent before starting the main rolling sequence.
  • Confirm the machine’s pre-bending capacity for the actual material, plate width and thickness; it can differ from its rolling capacity.
  • Where the required end curvature cannot be achieved directly, assess separate end forming or an allowance for trimming before cutting the blank.
  • Check the released shell at several positions, including the joint, rather than relying on one diameter measurement.
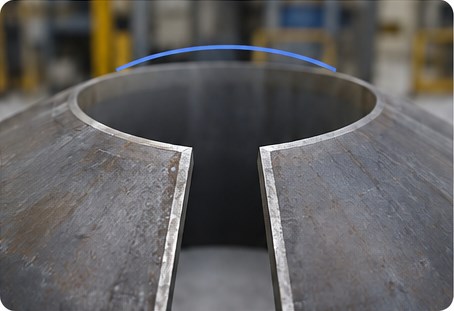
Flat ends at a rolled shell joint

Flat ends at a rolled shell joint

Extra pressure on the main body will not necessarily correct an end that lies outside the machine’s effective forming zone.

Tube and Pipe Bending: Diagnose Wrinkles, Flattening and Wall Thinning
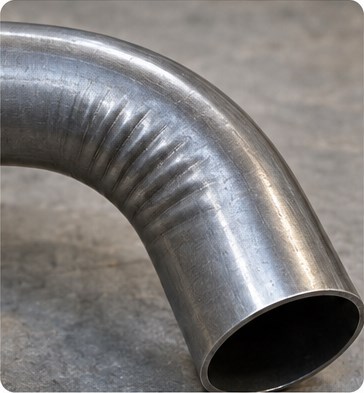
Bent steel tube showing wrinkles along the inside of the curve.

The challenge: The inside of the bend wrinkles while the outside flattens or becomes too thin.

  • Select the tooling using the tube diameter, wall thickness, material and bend radius together.
  • For rotary draw bending, assess whether an internal mandrel and a wiper die are required to support the tube.
  • Inspect mandrel position, tooling fit, lubrication and wear before changing forming pressures.
  • Distinguish wrinkles along the whole bend from a hump near its end: these can indicate different setup problems.

Increasing pressure is not a universal remedy. Excessive pressure-die force can contribute to outside flattening, so adjustments should follow the specific defect and tooling guidance.

Steel Section Bending: Protect the Cross-Section

The challenge: A beam, channel or angle reaches the required curve but develops flange distortion, web buckling or twist.

  • Show the bending axis and section orientation clearly on the drawing.
  • Use rolls shaped to support the profile, with supplementary restraints where needed to control local distortion.
  • Check the section shape and twist as well as the overall radius during forming.
  • If distortion remains unacceptable, review the required radius, section proportions and bending method with the designer before proceeding.
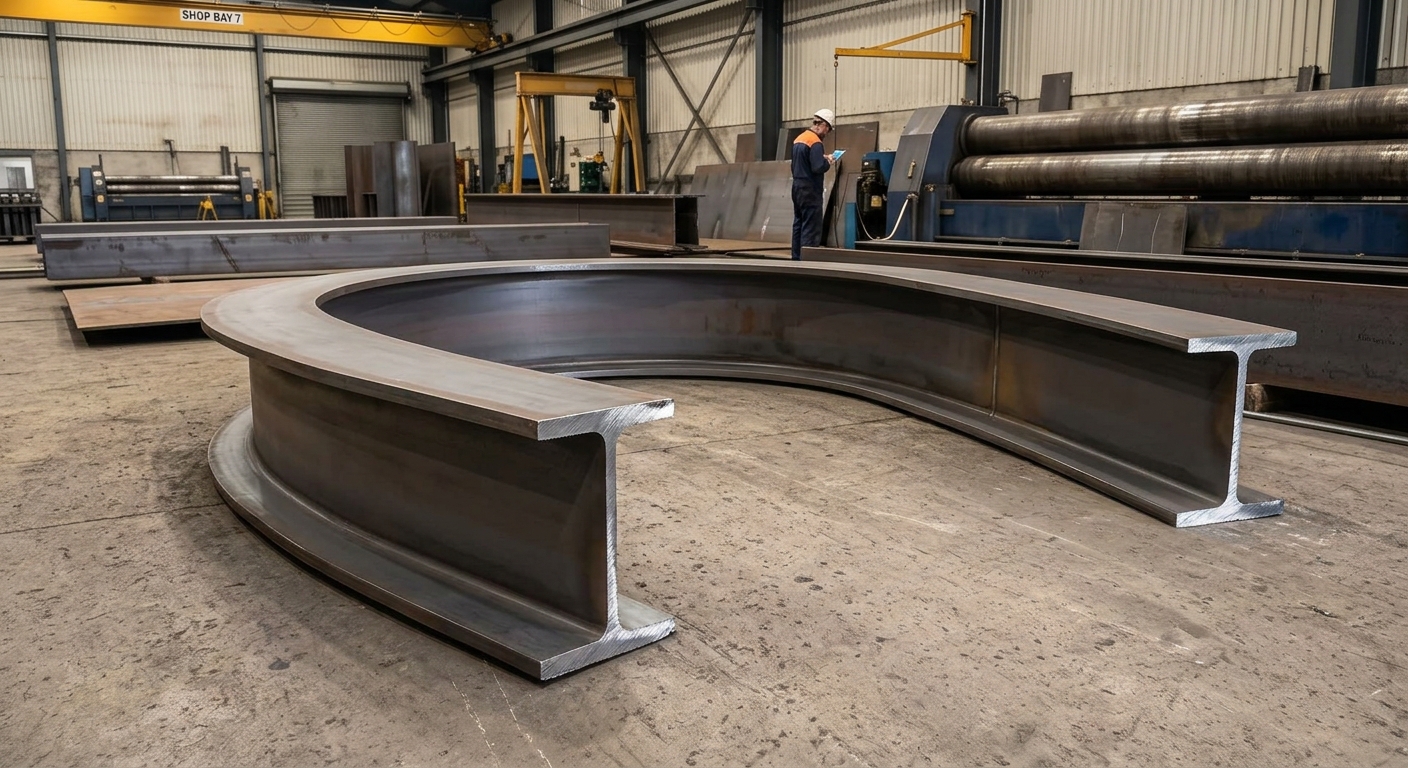
Curved Steel SEction

A section’s ability to reach a radius depends on its geometry and the support provided during bending.

Metal Stamping: Keep Material Flow Balanced

The challenge: Formed parts twist or dimensions drift during a production run, even though the drawing remains unchanged.

  • Keep blank positioning and lubricant application consistent.
  • Check die alignment, tool wear and the condition of features that restrain material flow.
  • Where blank holders are used, investigate uneven restraint if one side of a component deforms differently from the other.
  • Check dimensions after any trimming or piercing stages that may release residual stresses.

Inspect finished parts at planned intervals so changes in the process are detected before they affect the whole batch.

Deep Drawing: Balance Wrinkle Control Against Tearing
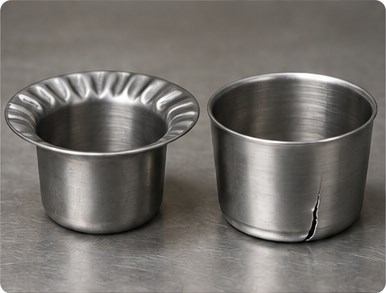
Two drawn steel cups showing flange wrinkles on the left and a wall tear on the right.

Flange wrinkles (left); wall tear (right).

The challenge: Increasing restraint removes wrinkles but causes thinning or splits elsewhere.

  • Review blank-holder pressure together with lubrication, tool radii and punch-to-die clearance.
  • If the flange wrinkles, check whether the blank is adequately and evenly restrained.
  • If the wall tears, investigate excessive restraint, poor lubrication, unsuitable radii or an excessive draw in one stage.
  • Consider multiple drawing stages where the required shape exceeds the material’s practical forming limits.

Assess wrinkles and wall thinning together during trials: a smooth-looking surface alone does not confirm an acceptable drawn part.

What to Include in a Steel Bending Enquiry

A useful steel bending enquiry defines the finished part, the order quantity and the condition required at delivery. Providing the same information to each supplier makes quotations easier to compare. Include:

  • Drawings and revision: identify the current drawing and ensure any accompanying model matches it.

  • Material and starting form: specify the steel grade, thickness or section size, and whether material is customer supplied.

  • Finished geometry: show the required shape, bend directions and dimensions that matter to assembly.

  • Quantity and ordering pattern: distinguish the immediate order from anticipated repeat demand.

  • Supply scope: identify whether the quotation should cover bending alone or include other requested operations, subject to supplier confirmation.

  • Acceptance requirements: state critical tolerances, surface expectations and any required inspection records or material documentation.

  • Delivery requirements: provide the destination, required date and any packaging constraints.

How can we help you ?

Novelty Structures uses advanced CNC Bending Machinery and techniques to fabricate custom steel bended parts. Whether you need precise sheet metal bending, pipe bending, or metal stamping, our contract fabrication serviced are tailored for various applications.

Contact our team to further discuss your needs.

Knowledge Hub