
Novelty Structures supplies CNC Precision (Swiss) Turning service for the manufacturing of precision turned components

Precision turning, also called Swiss turning, is a specialized CNC process perfect for creating small, detailed parts with high precision. Swiss Turning machines are designed to work with very tight tolerances and shorter production times than regular lathes, which makes them a great choice for producing complex parts efficiently and in larger quantities.
Precision (Swiss) Turning Materials
Metals

Plastics


Benefits of with Precision (Swiss) Turning

Precision Turned Products


Quality Control
Case Study 1: Slashing Cycle Times by Combining Operations
When producing small, high-volume parts, every second counts. Traditionally, manufacturers rely on multiple operations to finish a complex part—but this introduces intermediate handling, repositioning, and manual labour that drag down efficiency. By reviewing their complete manufacturing route and utilising a sliding-head turning centre, we dramatically transformed their production times.
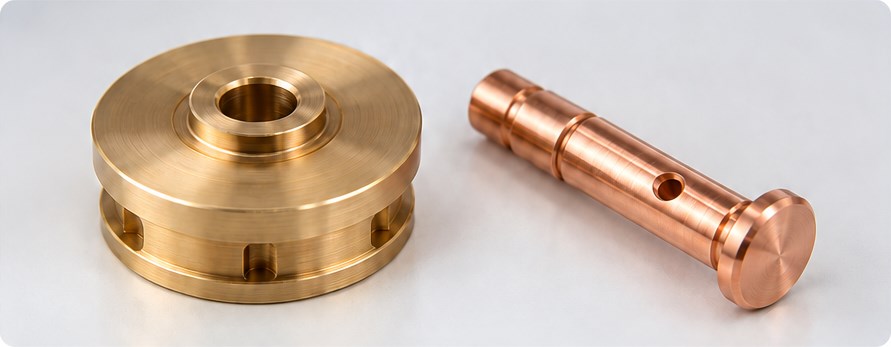
Bronze valve disc and copper linkage pin
The Transformation at a Glance
| Component | Previous Method | New Single-Cycle Method | Time Saved |
|---|---|---|---|
| Bronze Valve Disc (22mm dia. x 8 mm thick) | 2 machining operations taking 2.8 minutes | 1 operation taking 55 seconds (No intermediate handling) | ~67% faster |
| Copper Linkage Pin | 2 operations taking ~4.5 minutes, plus manual chamfering & stamping | 1 operation taking 95 seconds (Includes automated engraving) | ~65% faster |
Key Takeaways for Sourcing
Turning may only account for a fraction of the work. Repositioning, drilling, chamfering, and marking can heavily inflate your cost per component.
Case Study 2: Solving the "Rocking" Spacer Problem for an Automotive Client
A recent client approached us with a frustrating assembly issue. We were supplying a small, turned spacer designed to sit securely between a bracket and a mounting plate. During our initial QC checks, the overall length of the spacers matched their drawings perfectly. However, during the client’s final assembly, the spacers were rocking instead of sitting flat.
The Culprit: Parting-Off Burrs
We quickly identified that the issue stemmed from parting off—the operation that separates a finished component from the raw bar. This process was leaving a microscopic burr, or "pip," on the cut end. While tool geometry can be adjusted to reduce this, we knew that simply choosing a different insert involved a delicate trade-off between stability, face quality, and tool life
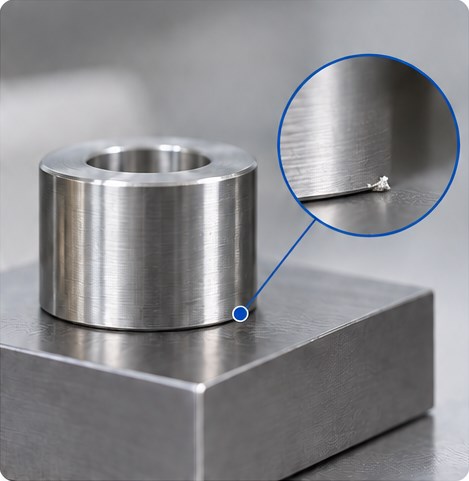
Spacer seating check
How We Solved It
Case Study 3: Overcoming Distortion in Thin-Walled Bushings
During an machinery component supply project, we manufactured a batch of, thin-walled aluminium bushings. While clamped inside our machines, the parts measured flawlessly. Yet, by the time they reached our quality control lab for final sign-off, the bores had distorted and fallen out of tolerance.
The Culprit: Clamping Pressure
Thin sections are highly susceptible to their environment. We realized that the work holding pressure required to keep the part stable during machining was temporarily squashing the component. Once released from the chuck, the metal sprang back into an oval, distorted shape.
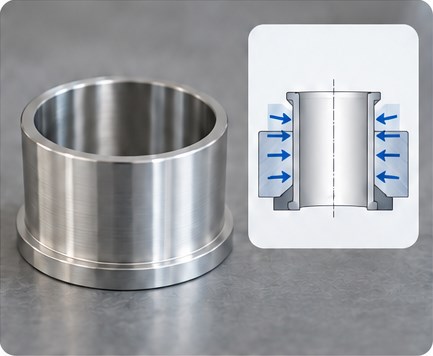
Thin-walled aluminium bushing
How We Solved It
Case Study 4: Fixing Threaded Fittings That Refused to Seat
We encountered a critical seating issue during a custom hydraulics project. Our CNC-turned threaded adapters had the exact correct nominal thread size, and they passed standard gauge checks. However, the client reported that during installation, the fittings stopped turning entirely before the shoulder could reach the intended seating face, preventing a watertight seal.
The Culprit: Incomplete Threads and Clearances
Our engineering team investigated and found a classic clearance clash. An incomplete thread profile directly next to the shoulder of the part was severely limiting how far the two components could physically engage.
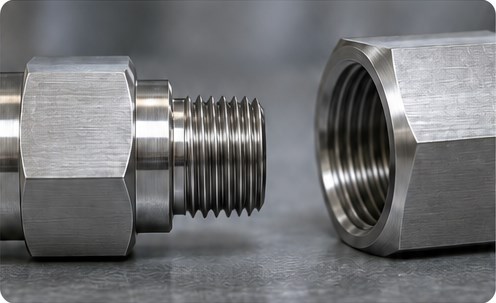
Threaded fitting mating parts
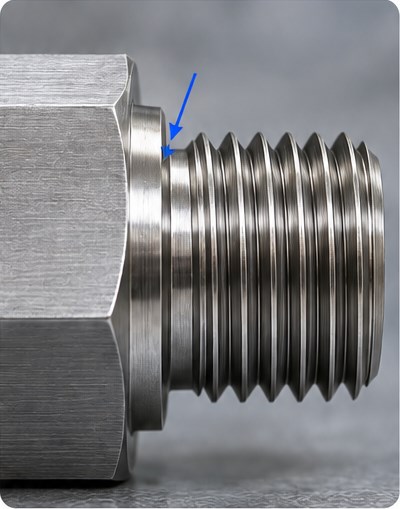
Thread relief at the shoulder
How We Solved It
How can we help you ?
Precision CNC turning services support various industrial applications, and selecting a suitable supplier is essential to successful production.
Novelty Structures supplies high-quality precision turned parts tailored to demanding industrial needs.
FAQ
CNC turning is perfect for creating parts like:
- Cylindrical components
- Screws and bolts
- Shafts and rods
- Bushings and spacers
- Threaded components
- Custom fittings
Turnaround time depends on the complexity of the part, quantity, and current workload. For simple parts, the lead time is usually 2-5 days, while complex or high-volume projects may take 1-2 weeks.
CNC turning is best suited for parts with rotational symmetry. However, features like grooves, threads, and complex contours can be added. Non-cylindrical designs may require additional CNC milling operations.
Pricing depends on factors like:
- Material type
- Part complexity
- Tolerances and surface finish requirements
- Quantity of parts
Yes, many CNC turning services offer secondary processes, including:
- Polishing
- Anodizing
- Plating (e.g., chrome or zinc plating)
- Heat treatment
- Surface grinding
- Lathes: Standard CNC lathes for basic turning operations.
- Swiss-style Lathes: For small, intricate parts.
- Multi-axis CNC Turning Centers: Combine turning and milling for complex parts in a single setup.
Yes, CNC turning can produce custom internal and external threads in both metric and imperial standards.
CNC turning can produce parts with varying surface finishes, such as:
- As-machined: Basic finish from the cutting tool.
- Polished: Smooth, reflective surfaces.
- Matte: Non-reflective surfaces.
- Bead blasting: For uniform textures.
- Anodizing or plating: For enhanced durability or aesthetics.
- 2-axis turning: Basic lathes for cylindrical and symmetrical parts.
- 3-axis turning: Adds a milling tool for additional features like slots or flat surfaces.
- Multi-axis turning: Combines turning and milling on multiple axes for complex, asymmetrical parts.
Modern CNC lathes with live tooling and multi-axis capabilities can handle complex geometries, including:
- Grooves and slots
- Undercuts
- Tapered or contoured surfaces
- Off-center holes
- Optimize part design to minimize complex features.
- Choose readily available materials.
- Order larger quantities to lower the cost per unit.
- Use tolerances only as tight as necessary for functionality.