
Contract CNC Turning Services and Custom Turned Parts Manufacturing
- Contract CNC Turning Services and Custom Turned Parts Manufacturing
- CNC Turning Service
- CNC Turning vs CNC Milling
- Turning Materials
- Quality Control
- Design for Turning
- Types of CNC Turning Machines
- Frequently Produced Products
- Advantages of CNC Turning
- CNC Turning Costs
- Case Studies: Optimizing CNC Turning Operations
- How can we help you ?
- FAQ
CNC Turning Service
In CNC turning, the cutting tool typically moves in a linear fashion while the work piece rotates. This is different from CNC milling, where the work piece is stationary while the cutting tool moves.
Turning is used to create a variety of shapes, including complex designs and geometries. It’s highly efficient for producing parts that are symmetrical around an axis of rotation. Major examples are as cones, cylinders, or shafts.

CNC Turning vs CNC Milling

Turning Materials
Metals

Plastics

Quality Control

Types of CNC Turning Machines

Frequently Produced Products



Case Studies: Optimizing CNC Turning Operations
In custom manufacturing and precision machining, solving production problems requires looking beyond just the machine time on paper. Below are three real-world projects where we helped separate clients overcome distinct technical and commercial hurdles—delivering higher quality, lower total costs, and reliable delivery timelines.
Case Study 1: Why Faster Machining Doesn’t Always Mean Cheaper Parts
Client Overview
A long-term automotive supplier routinely places repeat orders for high-volume turned pins.
The Challenge
To maximise throughput and keep part costs low, an aggressive machining approach was used to achieve the shortest possible cutting cycle time. However, this high speed created long, stringy swarf (metal shavings) that tangled around the tooling. Machine operator had to frequently stop the machine to clear the debris, and tangled metal occasionally scratched the critical surface finish of the parts, causing high rework and scrap rates.
Our Strategy & Solution
We re-evaluated the job using Total Batch Cost as our key metric—calculating the total expense of setup, machining, tooling changes, inspection, and rework divided by the number of accepted parts.
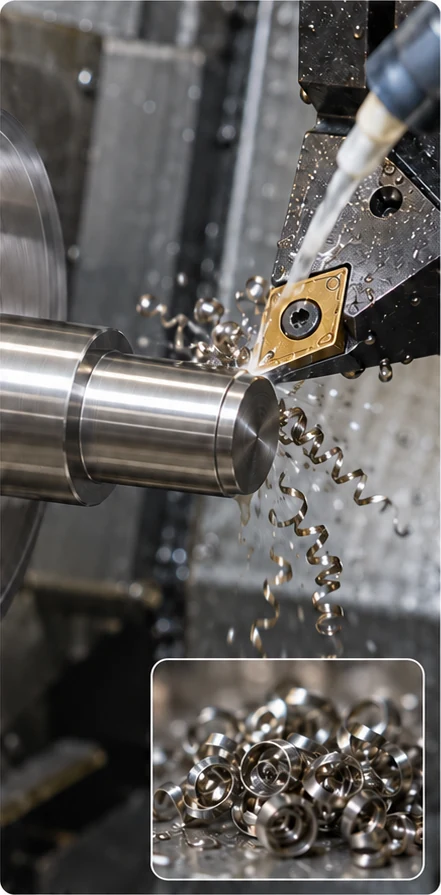
Turned pin chip control


Case Study 2: Preventing Assembly Delays by Proving Hard Features First
Client Overview
An industrial machinery manufacturer needed a batch of turned housings delivered for a scheduled assembly line launch.
The Challenge
While outer dimensions were straightforward, each housing required a deep internal bore designed to receive a tight-tolerance mating component. Due to the deep reach required, the boring bar experienced chatter and vibration marks inside the bore, preventing the mating component from fitting correctly. Discovering this issue during final inspection would leave only costly fixes—such as scrap or custom repairs—and risk shutting down the client’s assembly line.
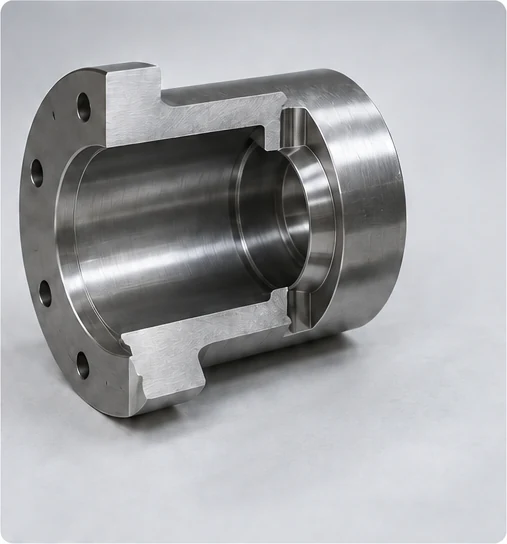
Deep-bore housing
Our Strategy & Solution
Rather than risking the full batch, we instituted a pre-production feature proving protocol:
- 1Stability Audit: We reviewed the boring bar’s overhang-to-diameter ratio, re-engineered the tool support rigidity, and optimized the cutting parameters specifically for deep-reach stability.
- 2First-Off Deep Inspection: We produced test pieces and thoroughly inspected the internal bore along its full working depth before releasing the remaining raw material for production.
- 3Risk vs. Cost Analysis: We presented the client with a clear decision point: investing a small, upfront process development fee to guarantee bore quality versus risking batch rework and assembly downtime.
Case Study 3: Lowering Setup Expenses Without Over-Stocking Inventory
Client Overview
An equipment brand needed several variations of turned spacers across multiple product lines.
The Challenge
The client required spacers that all shared the exact same material and outer diameter, but differed in length. Buying each part number on separate purchase orders meant paying repeated machine setup charges. However, ordering massive bulk quantities of every single length variant to avoid setup costs tied up too much capital in inventory.
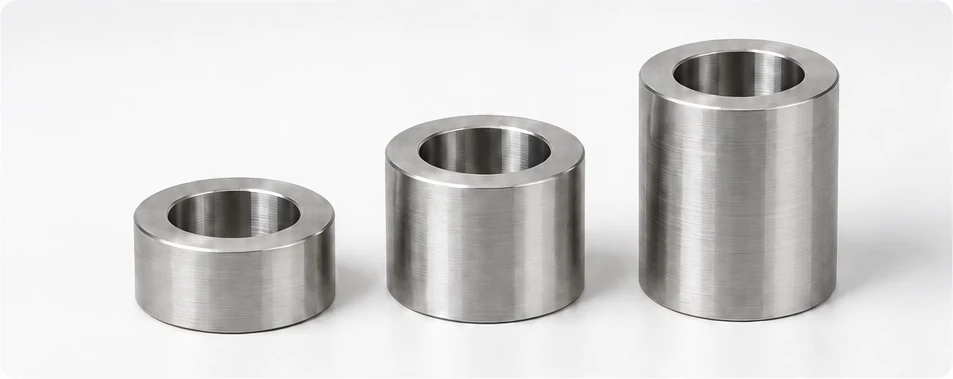
Turned spacer family
Our Strategy & Solution
We collaborated with the client’s purchasing team to group these individual line items into a Coordinated Part Family Campaign:
| Approach | Setup Costs | Inventory Capital | Overall Flexibility |
|---|---|---|---|
| Separate Purchase Orders | High (Paid per line item) | Low | High |
| Traditional Bulk Order | Low (One large setup) | High (Capital locked up) | Low |
| Our “Part Family” Strategy | Minimized (Shared setups) | Lean (Ordered to demand) | High (Staged delivery) |
How can we help you ?
Selecting a suitable CNC turning supplier is important to the success of industrial projects.
Novelty Structures provides high-quality custom CNC turned parts tailored to demanding industrial needs.
FAQ
CNC turning is perfect for creating parts like:
- Cylindrical components
- Screws and bolts
- Shafts and rods
- Bushings and spacers
- Threaded components
- Custom fittings
Turnaround time depends on the complexity of the part, quantity, and current workload. For simple parts, the lead time is usually 2-5 days, while complex or high-volume projects may take 1-2 weeks.
CNC turning is best suited for parts with rotational symmetry. However, features like grooves, threads, and complex contours can be added. Non-cylindrical designs may require additional CNC milling operations.
Pricing depends on factors like:
- Material type
- Part complexity
- Tolerances and surface finish requirements
- Quantity of parts
Yes, many CNC turning services offer secondary processes, including:
- Polishing
- Anodizing
- Plating (e.g., chrome or zinc plating)
- Heat treatment
- Surface grinding
- Lathes: Standard CNC lathes for basic turning operations.
- Swiss-style Lathes: For small, intricate parts.
- Multi-axis CNC Turning Centers: Combine turning and milling for complex parts in a single setup.
Yes, CNC turning can produce custom internal and external threads in both metric and imperial standards.
CNC turning can produce parts with varying surface finishes, such as:
- As-machined: Basic finish from the cutting tool.
- Polished: Smooth, reflective surfaces.
- Matte: Non-reflective surfaces.
- Bead blasting: For uniform textures.
- Anodizing or plating: For enhanced durability or aesthetics.
- 2-axis turning: Basic lathes for cylindrical and symmetrical parts.
- 3-axis turning: Adds a milling tool for additional features like slots or flat surfaces.
- Multi-axis turning: Combines turning and milling on multiple axes for complex, asymmetrical parts.
Modern CNC lathes with live tooling and multi-axis capabilities can handle complex geometries, including:
- Grooves and slots
- Undercuts
- Tapered or contoured surfaces
- Off-center holes
- Optimize part design to minimize complex features.
- Choose readily available materials.
- Order larger quantities to lower the cost per unit.
- Use tolerances only as tight as necessary for functionality.
Knowledge Hub